From tinplate to a fill-ready can.
在萨利赫利,一条产线完成全部工序。
We run cylindrical tin can production under one roof in Salihli (Manisa): slitting, forming, resistance welding, seaming and inspection are integrated into a single, high-volume flow.
Resistance-welded cylindrical bodies
We join can bodies by resistance (electric-resistance) welding. The overlapping side seam is made without solder and with low scrap, giving high strength and a tight seal. Rigidity beads, the flange and the bottom end are applied in our plant — we deliver the can fill-ready, with its bottom already seamed, together with its own easy-open end.
See how we control quality →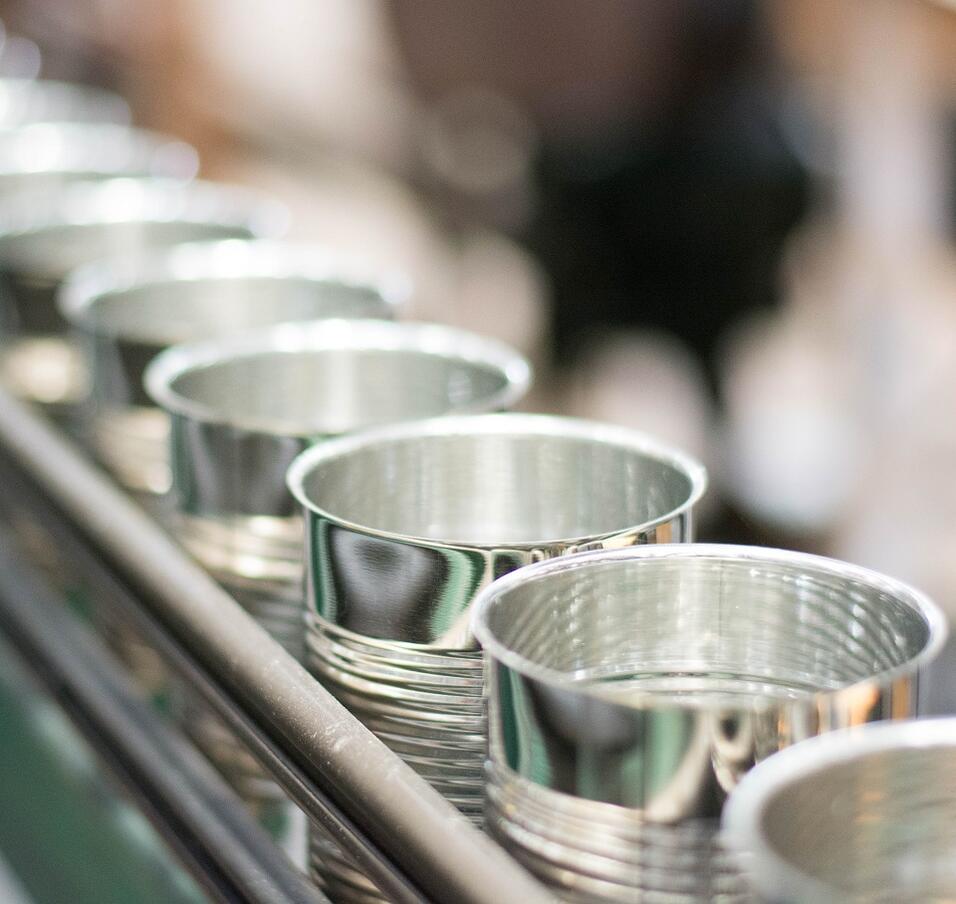
We share capacity and lead time specific to your project during our conversation.
Production process
Sheet preparation & slitting
Tinplate is slit to can size and prepared for the line.
Body forming
The flat sheet is rolled into a cylindrical body and positioned for welding.
Resistance welding (side seam)
The overlapping side seam is joined by electric-resistance welding, without solder.
Beading & flanging
Rigidity beads are formed and the flange is prepared for end seaming.
Bottom double seaming
The bottom end is closed in our plant with a controlled double seam — the can is fill-ready.
Leak & seam inspection
Cans are checked for leak-tightness and seam integrity.
Packing & dispatch
Cans are packed with their easy-open ends and dispatched.